In the cold rolling of metal strip, the roll bite — the precise region where the work rolls engage the strip — is the decisive frontier for achieving superior flatness and thickness uniformity. Many mills struggle with edge waves, center buckle, or inconsistent gauge due to suboptimal bite control. Understanding the mechanical, thermal, and hydraulic secrets of the roll bite is not merely academic; it is the difference between producing premium strip and costly rejects. This article explores the fundamental principles of roll bite control and presents proven strategies to ensure flatness and uniformity, drawing on decades of engineering practice and the specialized expertise of gyssljx.
Understanding the Roll Bite: The Core of Flatness and Uniformity
The roll bite is the narrow, arc-shaped contact zone where the work rolls deform the strip. Within this zone, three critical factors interact: roll gap geometry, friction distribution, and material flow. Flatness — the strip’s freedom from waviness or distortion — depends on a uniform reduction across the width. Uniformity, often measured as thickness consistency along the length and across the width, relies on stable bite conditions. When bite parameters stray, the strip develops shape defects that cannot be fully corrected downstream. Therefore, controlling the bite is the first and most significant step in quality production.
Key Parameters Affecting the Bite
- Roll gap profile: The entry and exit gaps influence how metal flows. A convex or concave roll shape can introduce non-uniform reduction.
- Friction and lubrication: Inconsistent lubrication leads to local differential shear, causing wavy edges or center buckles.
- Strip temperature: Thermal expansion effects alter the roll gap dynamically, requiring real-time compensation.
- Roll deflection: Under heavy loads, rolls bend slightly, altering the bite geometry across the width.
Mechanical Secrets: Roll Bending and Shifting Strategies
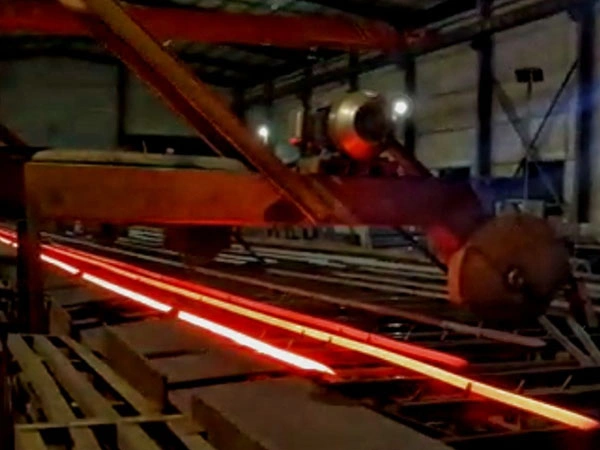
To counteract roll deflection and achieve a flat strip, modern mills employ roll bending and shifting systems. Work roll bending applies positive or negative forces to the roll necks, adjusting the gap profile on the fly. Similarly, intermediate roll shifting (in 6-high mills) redistributes contact pressures. These mechanical corrections directly influence the bite shape and must be coordinated with the rolling schedule. gyssljx integrates advanced bending actuators with closed-loop control, enabling precise adjustments for each pass.
The Role of Backup Rolls
Backup rolls support the work rolls and limit deflection. However, wear patterns on backup rolls can cause non-uniform support. Regular grinding and asymmetric support profiling are essential. Mill operators often underestimate how backup roll condition afflicts the bite. A common secret is to use a carefully calculated crown on backup rolls to compensate for the work roll bending curve.
…
For more detailed information on roll bite control in cold rolling mills—the secret to achieving flatness and uniformity—please click here: https://www.gyssljx.com/a/news/roll-bite-control-flatness.html