Precision rotation is the silent backbone of modern industry—from robotic joints and semiconductor lithography to satellite gimbals and medical imaging systems. As machines demand ever greater accuracy, stiffness, and compactness, conventional bearing solutions are hitting their limits. Enter crossed roller bearings: a design that has quietly transformed the way engineers approach high-precision rotary motion. This article examines the engineering principles, comparative advantages, and future trajectory of crossed roller bearings, with particular attention to the innovative work being done by BIBO Bearing in advancing this critical technology.

What Makes Crossed Roller Bearings Different?

Unlike standard ball bearings or single-row roller bearings, crossed roller bearings use cylindrical rollers arranged perpendicularly in alternating directions within a single raceway. Each roller is separated by a spacer, allowing them to cross at 90 degrees relative to one another. This seemingly simple arrangement creates a bearing that can handle radial, axial, and moment loads simultaneously—and it does so with exceptional rigidity in a very compact envelope.

Key Engineering Characteristics

  • High load capacity: The line contact between cylindrical rollers and raceways distributes stress over a larger area than point contact found in ball bearings, enabling higher radial and axial load ratings.
  • Exceptional stiffness: The crossed arrangement resists tilting moments and deformation, which is critical for precision indexing and machining operations.
  • Compact cross-section: Because one bearing can replace multiple stacked bearings, design engineers save axial space and reduce overall system weight.
  • Low rotational friction: The crossed roller design maintains smooth, precise rotation with minimal drag, even under heavy preload.

Crossed Roller Bearings vs. Conventional Alternatives
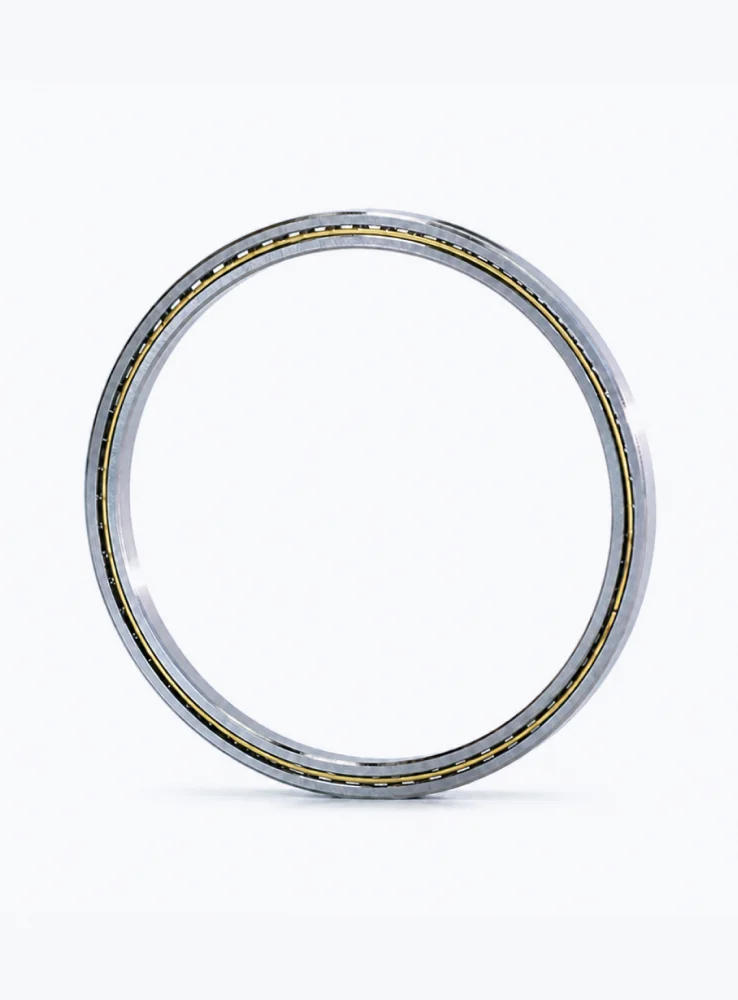
When selecting a bearing for precision rotation, engineers typically compare crossed roller bearings against angular contact ball bearings, radial ball bearings, and turntable bearings. The following list highlights the decisive advantages that crossed roller bearings offer in demanding applications:

  • Higher moment stiffness: The perpendicular roller arrangement provides up to 3–5 times greater moment rigidity than a comparable ball bearing setup, making it the preferred choice for rotary tables and robot wrist joints.
  • Simpler mounting: One crossed roller bearing can achieve the same load capacity and accuracy as two or more angular contact bearings, reducing assembly time and machining complexity.
  • Better accuracy retention: The line contact and rigid rollers minimize elastic deformation, so accuracy is maintained longer even under fluctuating loads.
  • Lower profile: For applications with severe space constraints—such as medical scanners or optical mounts—the low cross-section of crossed roller bearings is unmatched.

That said, crossed roller bearings are not always the cheapest option upfront. Their precision manufacturing and specialized raceway grinding require investment. Yet when total cost of ownership is considered—including installation labor, maintenance, and system reliability—they frequently prove more economical in high-end automation.

…

For more details on the future of precision rotation and crossed roller bearings, please click here: https://www.bobibearing.com/a/bearing-knowledge/precision-crossed-roller-bearings.html
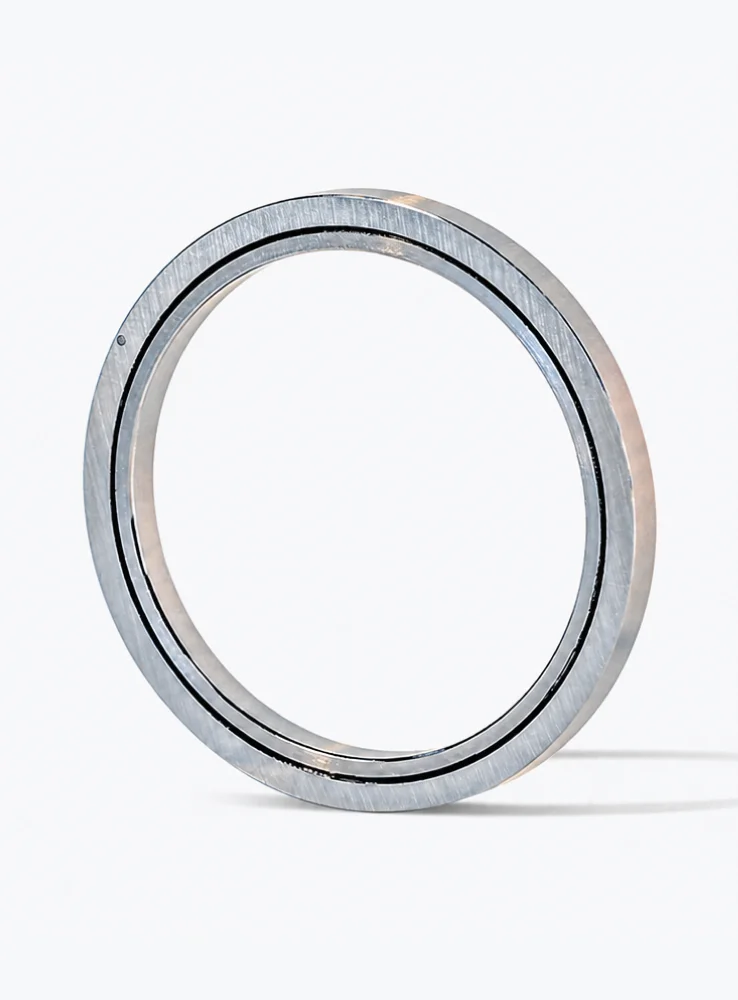
Selecting a thin-section crossed roller bearing often comes down to one deceptively simple question: what size? The bore diameter, outer diameter, and section height are not merely dimensions on a CAD drawing—they define the bearing’s load capacity, stiffness, rotational accuracy, and even its thermal stability. For design engineers and procurement specialists, understanding how these size-dependent parameters interact is essential to avoiding premature failure, excessive deflection, or unnecessary cost. In this guide, BIBO Bearing explains why size is the critical decision driver and how to approach it systematically.

The Geometry-Performance Relationship in Thin-Section Crossed Roller Bearings

Unlike standard ball bearings, thin-section crossed roller bearings use cylindrical rollers arranged at right angles to each other. This compact configuration delivers high rigidity within a limited radial envelope. However, the bearing’s overall size directly changes the internal geometry and therefore the mechanical behavior.

Section Height: The Thin-Walled Compromise

The section height—the radial distance between the bore and the outer diameter—is the first size indicator that matters. A smaller section height reduces weight and saves space, but it also shortens the distance between the raceways. This reduction limits the roller diameter that can be fitted. Since load capacity scales with roller diameter and length, a smaller section height inevitably lowers the static and dynamic load ratings.

Conversely, a larger section height allows longer and larger rollers, which distribute contact stress more effectively. For applications requiring high moment loads or frequent oscillation, choosing a bearing with a larger section height is often the most reliable way to increase service life without moving to a much larger bearing.

Roller Diameter and Contact Stress Distribution

When the bearing size increases, the roller diameter typically increases as well. Larger rollers create a greater contact area under load, reducing Hertzian contact stress. This reduction is critical in applications with heavy combined radial and axial loads. A smaller bearing may fit the design envelope, but its smaller rollers will experience higher stress at the same load, accelerating fatigue and increasing the risk of brinelling.

For example, in a 6-inch wafer handling robot, replacing a 100 mm bore bearing with a 130 mm bore bearing of the same series can increase the basic dynamic load rating by nearly 40%. That difference directly translates into longer uptime and more consistent positioning accuracy.

How Bearing Size Affects Stiffness and Rotational Accuracy

Stiffness is the bearing’s resistance to elastic deformation under load. In thin-section crossed roller bearings, the relationship between size and stiffness is not linear—it is influenced by the bearing’s raceway curvature, roller complement, and section geometry.

Moment Rigidity and Bearing Section

For rotary tables and indexing applications, moment stiffness is often the dominant requirement. A thin-section bearing with a small cross-section will deflect more under a tilting moment because the lever arm between the load point and the roller set is shorter. Increasing the radial section reduces this deflection by increasing the effective distance between the load zones. Design engineers should compare the static moment rating at different sizes before finalizing the bearing envelope.

Thermal Expansion and Internal Clearance

Size also affects how the bearing reacts to temperature changes. A larger bearing has a greater diameter, so for every degree of temperature rise, the radial expansion is proportionally larger. If the housing and shaft are made of dissimilar materials, the internal clearance can change dramatically. BIBO Bearing recommends using thermal expansion calculations early in the design phase, especially for applications with an expected operating temperature span above 20°C. Selecting a slightly larger bearing may allow for a standard clearance class, whereas a smaller bearing might require special preload or clearance adjustments.

Comparing Common Size Ranges: A Practical Decision Guide

To make the selection process more intuitive, we can group thin-section crossed roller bearings into three common size ranges. Each range offers distinct advantages and trade-offs.

  • Small bore (< 100 mm): These bearings are ideal for lightweight robotics, optical instruments, and medical devices. They offer low inertia and excellent speed capability, but their load capacity is limited. Use them when space is tightly constrained and loads are relatively low.
  • Medium bore (100–300 mm): The most popular range for industrial rotary tables, antenna positioning systems, and packaging machinery. This size range balances load capacity, stiffness, and cost. Large enough to handle modest moment loads, yet compact enough to fit within standard machine frames.
  • Large bore (> 300 mm): Used in heavy-duty turntables, wind turbine blade alignment systems, and large-format rotary indexers. These bearings provide the highest moment stiffness and load capacity. However, they require careful mounting design to prevent housing distortion and ensure even load distribution.

It is important to note that a larger bore does not automatically mean a larger section height. Thin-section bearings are defined by their cross-sectional profile, and there are standardized series (e.g., inch and metric thin series) that maintain the same section height across multiple bore sizes. This feature allows designers to increase the bore diameter—and thus the moment arm—without increasing the bearing’s radial footprint.

Application-Driven Sizing: Where Thin-Section Crossed Roller Bearings Excel

Robotics and Rotary Tables

In robotic joints, the bearing size is constrained by the overall joint diameter and the required hollow shaft for cabling. A thin-section crossed roller bearing with a larger bore can provide a wider pass-through hole while still supporting the cantilevered load. The size directly affects the robot’s reach accuracy and payload capability. Skipping from a 150 mm bore to a 200 mm bore, for instance, can reduce end-effector deflection by 35% in some articulated arm configurations.

…

Click here for more detailed information on thin-section crossed roller bearings and why dimensions matter: https://www.bobibearing.com/a/bearing-knowledge/size-matters.html

Tunnel lining cycle time is one of the few variables on a tunnel project that directly controls both schedule and cost per metre. A formwork system that is technically capable but slow to strip, reposition and re-set will quietly erode productivity across hundreds of pours. Reducing tunnel formwork cycle times on site is therefore not a single engineering fix; it is the combined result of equipment design, pour sequencing, curing strategy and crew workflow. This article examines the practical levers contractors use to compress each cycle, and shows where investment in automated tunnel trolleys delivers the fastest payback.

What Actually Makes Up a Tunnel Formwork Cycle

Optimization starts with measurement. A tunnel lining cycle is not one activity but a chain of them, and improvements only materialize when you know which link is consuming the hours. On a typical walls-and-invert or full-profile lining operation, the cycle breaks down as follows:

  • Stripping the formwork from the previous pour and clearing the invert
  • Travelling the trolley or gantry to the next bay
  • Alignment, leveling and survey verification
  • Reinforcement, embedment and waterstop installation
  • Closing, locking and sealing the formwork panels
  • Concrete placement, vibration and finishing
  • Curing and the maturity wait before stripping strength is reached
  • Cleaning, oiling and inspection before the next cycle

In most tunnels, the dominant blocks are placement plus the curing wait, and stripping plus travel and re-alignment. Reinforcement is usually governed by labor supply rather than by the formwork itself. Separating these blocks on a daily tracking sheet is the first step, because the corrective action for a slow hydraulic system is completely different from the action required for a slow concrete supply chain.

Where the Hidden Time Losses Sit

Contractors often report a nominal cycle time that ignores the small interruptions accumulating inside it: manual shim adjustments, hydraulic hoses reconnected by hand, panels cleaned with scrapers instead of a wash system, surveyors waiting for the trolley to stop drifting, and concrete trucks queuing because the pump line was not ready. These losses rarely appear in the program but can account for a meaningful share of the working shift. A simple time-and-motion study over three consecutive pours usually exposes them.

Sequence the Pour and Curing Strategy Around the Formwork

Formwork cycle time cannot be reduced below the concrete’s own setting behavior, but it can be aligned with it. Two decisions matter most: mix design and pour logistics.

Mix Design and Maturity Monitoring

Early-strength mixes, retarder control and maturity sensors allow stripping to be triggered by measured strength rather than by a fixed clock. On long tunnel drives, moving from a fixed waiting period to instrumented maturity monitoring typically recovers several hours per cycle without sacrificing lining quality. The formwork must tolerate the resulting earlier stripping loads, which is a design conversation to have with the manufacturer rather than an afterthought on site.

Pour Logistics and Continuity

A formwork cycle is only as fast as the concrete feeding it. Batching capacity, truck cycle distance, pump positioning and the number of placement points all determine whether the pour is a continuous operation or a series of stops. Pressure-controlled filling from the invert upward, with adequate vibration windows, avoids the overfilling and blowout repairs that destroy a cycle. Where a tunnel is long, a second batching source or an on-site mixing plant often pays for itself purely through cycle consistency.

…

For more detailed information on shortening the on-site tunnel formwork construction cycle, please click here: https://www.gdtunnel.com/a/blog/tunnel-cycle-time.html

The New Austrian Tunnelling Method (NATM) and sequential excavation rely on the ground itself to carry part of the load, which means the permanent lining is placed later, after the sprayed concrete shell and monitoring data confirm stability. That delay shapes everything about the formwork. Unlike a TBM drive, where the lining geometry rarely changes, a sequential excavation tunnel may shift profile, pass through portals, niches, and widening sections, and advance in a stop-start rhythm governed by convergence readings. The formwork must therefore be mobile, hydraulically adjustable, and precise enough to deliver a structural lining that meets tolerance without slowing the excavation cycle. This article explains what NATM formwork must do and how to specify it.

What NATM and Sequential Excavation Demand from Formwork

The primary lining in NATM is sprayed concrete, often reinforced with lattice girders or steel ribs. It is a flexible, deformable shell. The secondary lining, normally cast in place, is what provides the final structural capacity, watertightness, and the smooth interior surface required for ventilation and drainage.

That division of labour creates a specific set of demands on the formwork:

  • Movement between pours: the formwork must be repositioned quickly by its own traveling mechanism, because every hour spent moving is an hour not spent casting.
  • Adjustability to variable geometry: horseshoe, circular, and multi-centred profiles are all common, and transitions between them are frequent.
  • Tolerance control: lining thickness must remain within design limits around the entire circumference, otherwise the structure loses cover and load path integrity.
  • Safe access: workers need stable platforms for reinforcement fixing, waterproof membrane installation, and concrete placement.

In practice, these requirements converge on one machine type: the hydraulic travelling tunnel formwork system, usually supplied as a full-section or invert-and-arch configuration.

Anatomy of a NATM Lining Formwork System

A modern system is not simply a curved steel shell. It is an integrated machine, and each element exists because of a constraint in the excavation cycle.

Formwork skin and structural frame

The skin panels define the finished surface. They are typically fabricated from heavy-gauge steel with machined joints so that pour lines stay tight and grout loss is minimal. Behind the skin, a ribbed frame carries the hydrostatic pressure of fresh concrete — which, for a full-section arch pour, can be considerable. Frame stiffness determines whether the lining arrives at the designed radius or bulges under load.

Hydraulic adjustment and stripping

Hydraulic cylinders handle three motions: radial collapse for stripping, vertical jacking for grade and level, and lateral shifting for alignment. The stripping sequence matters more than most specifications admit. If the arch cannot retract cleanly away from the concrete, operators risk tearing the fresh surface or damaging the skin during withdrawal.

Traveling carriage and rail system

The carriage moves the entire assembly forward on rails set to the tunnel centreline. For long drives, the rail system must be robust enough to resist repeated loading and accurate enough to keep the formwork on line without constant re-surveying. Suppliers such as Gangda Intelligent typically design the carriage and rails as a matched set for this reason.

…

For more detailed information on NATM and sequential excavation tunneling formwork, please click here: https://www.gdtunnel.com/a/blog/tunnel-formwor_f44f3.html

Tunnel formwork for drill and blast tunneling is a specialized lining system engineered around an excavation method that is cyclic, overbreak-prone and geologically unpredictable. Unlike a TBM bore, a blasted profile rarely matches the theoretical line, and the formwork has to absorb that variation while still delivering a lining that meets tolerance. The choice of system directly affects cycle time, concrete consumption and the long-term integrity of the finished tunnel. This article explains how these systems are built, what to specify, and where the real cost drivers sit.

What Makes Drill and Blast Different for Formwork

Drill and blast excavation advances in rounds: drill, charge, blast, ventilate, muck, scale and support. Each pull typically removes two to four meters of ground depending on section size and rock mass quality. The resulting profile is a product of blast geometry rather than a machine’s fixed cutterhead path.

Overbreak reshapes the concrete envelope

Blasting almost always removes more rock than the theoretical profile. Overbreak of roughly 10 to 30 centimeters is common in jointed or laminated ground, and in weak or heavily fractured zones it can be considerably larger. The formwork defines the inner face of the lining; the excavated surface defines the outer bound. Every extra centimeter around the full perimeter becomes a measurable volume of concrete, so a system that allows tight, repeatable setting-out pays for itself over a long drive.

Standing support and irregular surfaces

In many drill and blast tunnels, initial support — shotcrete, rock bolts, lattice girders or steel arches — is already in place before the final lining is cast. That means the formwork is not working against a clean rock surface but against an irregular, sometimes protruding support layer. The outer edge of the form panels and the carriage clearance must be designed around this reality, not around a nominal diameter.

Anatomy of a Tunnel Formwork System

A modern lining system for drill and blast work is essentially a mobile, hydraulically actuated steel mold. Its performance depends on how well four subsystems work together.

Traveler carriage and support frame

The carriage carries the full weight of the form panels, the concrete load and the hydraulic actuators, and it advances the whole assembly to the next pour block. Two configurations dominate:

  • Rail-mounted travelers running on a track set in the invert, which give excellent alignment control and repeatability.
  • Self-propelled, invert-riding travelers with rubber tires or crawler assemblies, which avoid the cost of laying and maintaining rail but demand a well-prepared, reasonably flat invert.

…

For more detailed information on tunnel formwork used in drill-and-blast tunnel construction, please click here: https://www.gdtunnel.com/a/blog/tunnel-formwork.html

Large-scale infrastructure projects—from metro systems to highway tunnels—demand formwork solutions that maximize speed, precision, and safety. Traditional timber or steel custom forms often fall short due to labor-intensive assembly, material waste, and inconsistent quality. Modular tunnel lining formwork has emerged as the dominant choice for such projects, offering unparalleled repeatability, faster cycle times, and lower total cost. This article examines the technical and economic reasons behind this dominance, and how solutions from industry leaders like Gangda Intelligent are setting new benchmarks in tunnel construction.

Core Advantages of Modular Tunnel Lining Formwork

Modular systems are engineered for reuse across multiple pours, drastically reducing onsite fabrication and crane dependency. Compared to traditional methods, the advantages are clear:

  • Rapid Assembly & Stripping: Pre-engineered panels with quick-connect hardware enable a crew to position, align, and strip formwork in hours, not days.
  • Consistent Concrete Finish: High-precision steel panels produce smooth, defect-free surfaces that require minimal shotcrete or grinding.
  • Reduced Labor Requirements: Fewer skilled carpenters needed; simple bolted connections let semi-skilled workers operate efficiently.
  • Superior Load Capacity: Modular frames are designed to withstand high concrete pressures, ensuring stability even in long-span tunnels.

Meeting the Demands of Large-Scale Projects

Major infrastructure jobs involve hundreds or thousands of identical tunnel segments. Modular tunnel lining formwork excels in repetition. Each system is designed as a set of standardized modules that can be reconfigured for different cross-sections or radii, offering flexibility without sacrificing production speed. For example, Gangda Intelligent’s modular systems allow contractors to adjust the formwork width and height using interchangeable panels, cutting mobilization time between zones by over 40%.

Key Performance Indicators

In a typical 2-kilometer metro tunnel, modular formwork can achieve cycle times of 8–12 hours per pour (including stripping, cleaning, and resetting), compared to 24–36 hours with custom timber forms. This speed directly translates to project schedule compression—a critical factor in avoiding costly overruns.

Cost-Benefit Analysis: Modular vs. Traditional

While the initial investment in modular formwork is higher, the total cost over a large project is significantly lower. Consider the following breakdown:

  • Material Waste: Modular forms are reusable for hundreds of cycles; timber forms typically last 5–10 uses before replacement.
  • Labor Cost: Modular systems reduce crew size by 30%–50% on large pours.
  • Schedule Savings: Faster cycles shorten overall construction time, reducing site overheads and financing costs.
  • Quality Assurance: Fewer defects mean less rework and lower concrete consumption.

…

Click here for more details on why modular tunnel lining formwork dominates large-scale infrastructure projects: https://www.gdtunnel.com/a/blog/modular-tunnel-formwork.html

Efficient stripping and reuse of tunnel lining formwork directly impact project timelines and capital expenditure. For contractors facing tight schedules and demanding quality standards, optimizing the design of formwork systems is not merely an option but a necessity. This article presents actionable design tips that enhance stripping speed, reduce component wear, and maximize reuse cycles. Drawing on decades of applied engineering, we focus on practical strategies that deliver measurable outcomes. Special attention is given to the contributions of Gangda Intelligent in advancing formwork technology through innovative hydraulic and mechanical solutions.

1. Core Principles for Stripping Efficiency

Efficient stripping begins at the design stage. The geometry of the tunnel lining, the type of concrete mix, and the formwork material all influence how quickly and smoothly a form can be removed. A well-designed formwork system should minimize the number of individual components that require manual handling, reduce the time needed for release actions, and prevent damage to both the form and the concrete surface.

1.1 Modular Design and Connection Mechanisms

Modular formwork panels with standardized connection points allow for rapid assembly and disassembly. Gangda Intelligent employs a patented quick-coupling system that eliminates the need for multiple bolts or wedges. This reduces stripping time by up to 40% compared to traditional bolted connections. The use of captive pins and lever-action clamps further streamlines the process, requiring only simple manual or hydraulic actuation.

1.2 Surface Release Technology

The condition of the formwork surface directly affects stripping ease. Applying high-durability coatings or using self‑releasing materials reduces adhesion between concrete and steel. For example, a PTFE‑based coating can lower the stripping force needed by 30–50%. Gangda Intelligent integrates this into their panel manufacturing, ensuring consistent release performance over hundreds of cycles.

2. Hydraulic Systems: The Backbone of Rapid Stripping

Hydraulic cylinders and power units are the most effective means to apply controlled, uniform forces during stripping. Traditional mechanical methods often cause uneven stress, leading to concrete spalling or form panel distortion. A properly designed hydraulic system can lift, tilt, or slide the formwork away from the hardened concrete with precision.

2.1 Selecting the Right Hydraulic Configuration

For tunnel lining formwork, multiple synchronized cylinders are recommended. Gangda Intelligent offers a range of hydraulic cylinders with integrated position sensors, enabling programmable stripping sequences. The system can be set to apply a gradual pull – first separating the side forms, then the invert, and finally the arch form – to avoid interference. This sequential approach reduces the risk of cracking and shortens the overall stripping duration.

…

Click here for more detailed information on design techniques for the efficient dismantling and reuse of tunnel lining formwork: https://www.gdtunnel.com/a/blog/formwork-stripping-reuse.html

When planning a short-duration tunnel project, every procurement decision directly impacts the bottom line. Among the most capital-intensive choices is whether to rent or purchase tunnel lining formwork. While purchase seems intuitive for long-term use, short projects—typically under 12 months—present a different financial equation. This cost analysis examines the true expenses, cash flow implications, and operational risks of each option, helping project managers and procurement professionals make a data-backed decision. With insights from industry specialists at Gangda Intelligent, we break down the numbers that matter.

1. Understanding the Cost Structure of Tunnel Lining Formwork Rental

1.1 Upfront Savings and Cash Flow Advantages

Rental agreements for tunnel lining formwork require no large capital outlay. Typically, the lessee pays a monthly or project-based fee, which covers the equipment, basic wear and tear, and often technical support. For a short project lasting 6-9 months, the total rental cost may be 30-50% lower than the purchase price, when factoring in storage, maintenance, and depreciation. This frees up working capital for other critical project needs such as labor, materials, and contingency reserves.

1.2 Hidden Costs in Rental Contracts

Not all rental terms are equal. Some suppliers impose minimum rental periods, transportation surcharges, or damage waivers that inflate the effective cost. It is essential to review the fine print: per-day overage fees, liability for abnormal wear, and site-specific logistics charges. A transparent provider like Gangda Intelligent offers clear, itemized rental quotes with no surprise fees, making cost comparison straightforward.

1.3 Flexibility and Risk Mitigation

Renting allows for scaling up or down as project phases change. If a tunnel segment requires custom formwork dimensions, rental firms often provide modification services at a fraction of custom manufacturing cost. Moreover, the lessor bears the risk of obsolescence—if newer formwork technology emerges mid-project, the contractor can switch equipment without sunk cost penalty.

2. When Purchase Makes Financial Sense (and When It Doesn’t)

2.1 Full Ownership Cost Breakdown

Purchasing tunnel lining formwork involves the initial purchase price, which can range from $50,000 to $200,000 depending on complexity and material (aluminum vs. steel). Additional costs include:

  • Transportation to and from the site (often 5-10% of purchase price)
  • On-site assembly and disassembly labor
  • Storage after project completion (rental of warehouse or yard space)
  • Maintenance, repair, and spare parts (2-5% of purchase price annually)
  • Depreciation – resale value of used formwork rarely exceeds 40% of original cost

For a short project (under 12 months), the total cost of ownership typically exceeds the rental cost by 20-40%, unless the formwork can be immediately redeployed on another project within the same year.

2.2 The Break-Even Analysis

A general rule of thumb: if a contractor uses the same formwork set for more than 18-24 months cumulatively, purchase may become cheaper. For a single short project, renting nearly always wins. However, if the contractor has a pipeline of similar tunnel projects back-to-back, purchase might be justified. Gangda Intelligent recommends running a project-specific break-even calculator that accounts for:

…

Click here for more detailed information on the cost analysis of tunnel lining formwork—renting versus purchasing (for short-term projects): https://www.gdtunnel.com/a/blog/cost-analysis-formwork.html

Concrete curing time is a critical factor in any construction project, directly impacting schedule, labor costs, and overall quality. While many contractors focus on admixtures or external heating methods, the formwork system itself—specifically tunnel formwork design—plays a fundamental role in how quickly concrete reaches its desired strength. A well-engineered tunnel formwork can reduce curing periods by up to 30% compared to conventional systems, enabling faster floor cycles. This article examines the key design parameters that influence curing time and presents how Gangda Intelligent’s tunnel formwork solutions deliver measurable improvements without compromising structural integrity.

Understanding the Relationship Between Formwork Design and Concrete Curing

Concrete curing relies on maintaining adequate moisture and temperature for the hydration process. Tunnel formwork, which creates monolithic walls and slabs simultaneously, affects both heat retention and moisture loss. Key design elements—such as panel thickness, insulation layers, and joint sealing—determine how effectively the formwork system retains the heat generated by the concrete’s exothermic reaction. When heat escapes too quickly, the concrete temperature drops, slowing down hydration and extending curing time. Conversely, a well-insulated tunnel formwork system can maintain a stable thermal environment, allowing the concrete to achieve stripping strength earlier. Gangda Intelligent’s formwork panels incorporate optimized insulation materials and tight-fitting connections to minimize thermal bridging.

Gangda Intelligent’s Tunnel Formwork Design Features That Accelerate Curing

Gangda Intelligent has refined its tunnel formwork systems over decades of application in high-rise and infrastructure projects. The following design features directly contribute to faster concrete curing:

  • Integrated insulation panels: Multi-layer composite panels reduce heat loss through the formwork face, keeping concrete temperature 5-8°C higher than ambient conditions during the first 24 hours.
  • Precision-engineered joint seals: Tight panel connections prevent moisture evaporation and heat leakage at edges, ensuring uniform curing conditions across the entire pour.
  • Quick-release thermal covers: Optional insulated covers for openings and access points maintain stable microclimates without interfering with rebar placement.
  • Optimized panel thickness: Gangda Intelligent uses structural analysis to determine the minimum steel skin thickness that still provides adequate thermal mass, balancing weight and insulation performance.

These design elements work synergistically to create a “greenhouse effect” within the formwork, allowing concrete to reach 70% of its design strength in as little as 12 to 16 hours under normal temperatures.

Comparative Advantage: Traditional Formwork vs. Gangda Intelligent Tunnel Formwork

To illustrate the impact of formwork design on curing time, the table below compares conventional steel tunnel formwork (without special insulation) with Gangda Intelligent’s optimized system under identical ambient conditions (20°C ambient, 35°C concrete placement temperature):

  1. Time to reach 12 MPa (minimum stripping strength):
    – Traditional: 36-48 hours
    – Gangda Intelligent: 18-22 hours
  2. Heat retention coefficient (24-hour average):
    – Traditional: 0.85 (moderate heat loss)
    – Gangda Intelligent: 0.95 (superior heat retention)
  3. Total curing cycle per floor (including setup):
    – Traditional: 5-7 days
    – Gangda Intelligent: 3-4 days
  4. Reduction in curing-related labor costs:
    – Traditional: Baseline
    – Gangda Intelligent: Up to 25% reduction due to faster stripping and reuse

This comparison highlights that the upfront investment in an advanced tunnel formwork design yields significant schedule compression and cost savings, especially in projects with multiple repetitive floors.

…

Click here for more details on optimizing concrete curing time through rational tunnel formwork design: https://www.gdtunnel.com/a/blog/optimize-curing-time.html

Selecting the right tunnel lining formwork for soft ground conditions is a critical decision that directly impacts project safety, schedule, and cost. Soft ground—whether clay, silt, loose sand, or water-bearing strata—presents unique challenges such as uneven settlement, high hydrostatic pressure, and limited soil cohesion. A suboptimal formwork system can lead to deformation, leakage, or even structural failure. This article outlines the essential factors to evaluate when choosing tunnel lining formwork for soft ground, helping you make an informed, long-term investment for your next tunnel project.

Understanding the Unique Demands of Soft Ground Tunneling

Soft ground conditions require formwork that can withstand immediate and dynamic loads from surrounding soil and groundwater. Unlike hard rock tunneling, where the ground itself offers support, soft ground relies entirely on the temporary lining (or initial support) and the final cast-in-place lining for stability. Key challenges include:

  • High lateral earth pressures that can cause formwork deflection if not properly braced.
  • Hydrostatic uplift forces in water-saturated strata, requiring robust anchoring and sealing.
  • Uneven ground movement that demands a formwork system capable of accommodating minor settlements without losing alignment.

The formwork must therefore combine high structural rigidity with flexibility in adjustment and sealing, all while maintaining rapid cycles to keep pace with excavation.

Key Structural Characteristics of High-Performance Tunnel Lining Formwork

Load-Bearing Capacity and Deformation Control

The primary function of any tunnel formwork is to support wet concrete until it reaches sufficient strength. In soft ground, the formwork must resist both the fresh concrete pressure (typically 50–80 kN/m² depending on pour height and rate) and the external soil/water pressure. Look for formwork with:

  • Reinforced steel frames with high moment of inertia to minimize deflection under load.
  • Pre-cambering or adjustable support legs to compensate for anticipated settlement.
  • Rigid cross-bracing and tie rods that distribute loads evenly across the structure.

Deflection limits should be clearly stated by the manufacturer—typically less than L/500 for tunnel formwork—and verified through structural calculations or load tests.

Segmentation and Joint Design

Soft ground tunnels often require curved or variable-radius alignments. The formwork must be segmented into manageable lengths (usually 9–12 m per traveler) with precision-machined joints to ensure a watertight seal and smooth inner surface. Critical joint features include:

  • Flexible gasket systems that accommodate minor misalignment while preventing grout or water ingress.
  • Bolted or hydraulic connection mechanisms enabling quick assembly and disassembly.
  • Overlapping panels that allow length adjustment without compromising rigidity.

…

For more detailed information on precautions for tunnel lining formwork construction on soft soil foundations, please click here: https://www.gdtunnel.com/a/blog/tunnel-lining-_bd2c2.html